How Does CNC Turning Milling Compound Processing Improve Manufacturing Efficiency?
2026-10-29
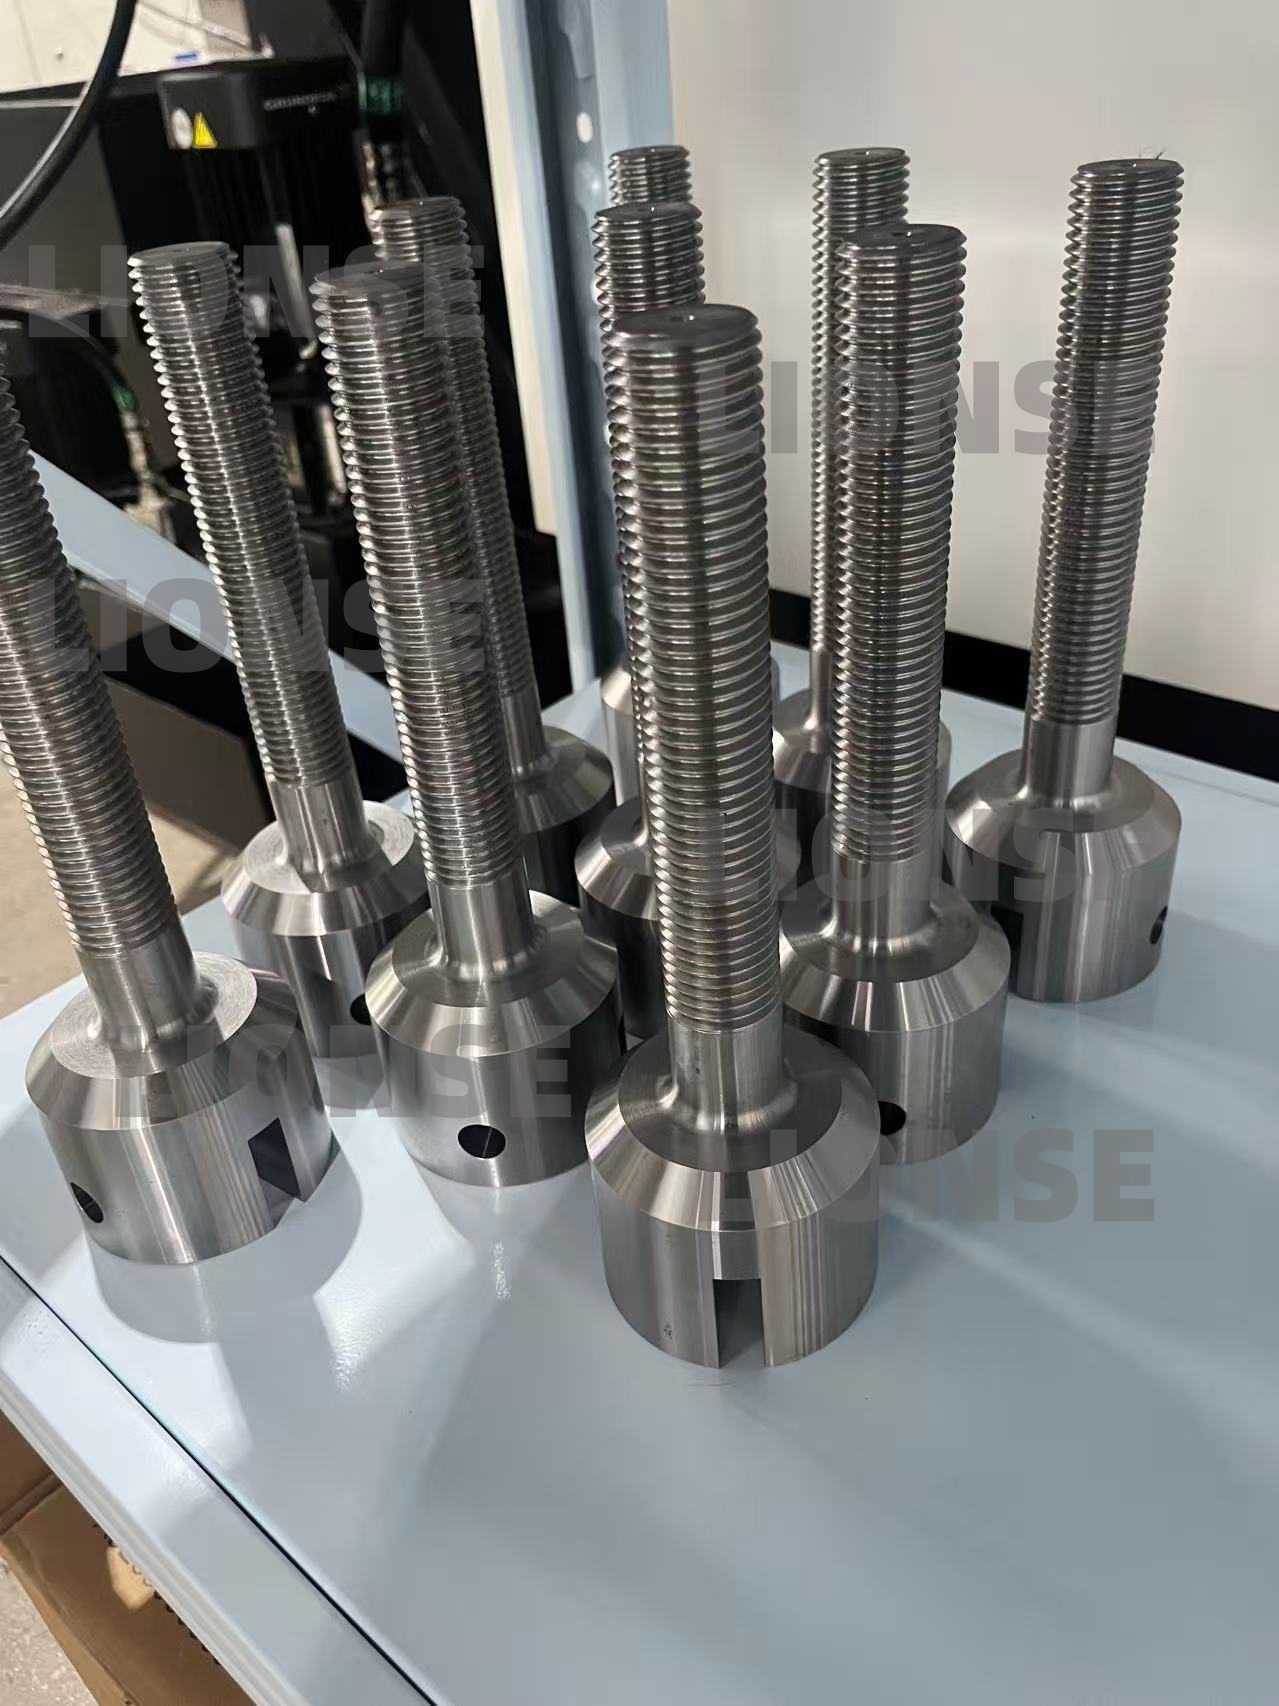
A shop manager quotes a valve body that requires a turned outside diameter, a milled mounting pad, four drilled holes, and an internal groove. The traditional route uses a lathe for the turning and a machining center for the milling. The part is clamped twice, and the second clamping must be aligned to the first. The shop manager compares this route with CNC Turning Milling Compound Processing, where the same part is completed in one setup on a turn-mill machine. The compound route removes one clamping, one alignment, and one queue between machines. The result is a shorter lead time and a tighter tolerance on the relationship between the turned features and the milled features. This guide explains how the compound process improves manufacturing efficiency.
1. Why Does the Traditional Two-Machine Route Lose Time and Accuracy on Complex Parts?
The traditional route separates turning and milling into two operations on two machines. Each operation requires a separate setup, a separate program, and a separate inspection. The part must be unclamped from the lathe, transported to the machining center, and clamped again in a different fixture. Each clamping introduces a new datum. The second operation is aligned to the first, but the alignment is never perfect. The error from the second clamping is added to the error from the first. The queue between the two machines also adds to the lead time. For a batch of 200 parts, the queue can add two to five days. In our factory, we operate both the traditional route and the compound route. Qingdao Lionse Mechanical Engineering Co., Ltd. has been machining precision parts for over 12 years.
The accuracy loss is most visible on features that must be coaxial or perpendicular. If a bore is turned in the first operation and a face is milled in the second operation, the perpendicularity between the bore and the face depends on the second clamping. The compound process keeps the part in one clamping, so the relationship is controlled by the machine geometry, not by the fixture.
2. How Does a Single Setup Eliminate the Benchmark Transfer Error?
In CNC Turning Milling Compound Processing, the part is clamped once in the main spindle. The turning tools and the driven tools work from the same machine coordinate system. The turret or the B-axis head moves in the same linear axes that position the turning tools. The milled features and the turned features are therefore referenced to the same datum. The benchmark transfer error, which is the error introduced when the part is re-clamped in a second fixture, is eliminated. The table below compares the two routes for a typical part with a coaxial bore and a milled pad.
| Parameter | Two-machine route | Compound route |
| Number of clampings | 2 | 1 |
| Coaxiality (bore to OD) | 0.03 – 0.05 mm | 0.01 – 0.02 mm |
| Perpendicularity (pad to bore) | 0.04 – 0.06 mm | 0.015 – 0.025 mm |
| Setup time per batch | 3 – 4 hours | 1 – 1.5 hours |
| In-process waiting | 2 – 5 days | None |
In our factory, we measure the coaxiality and perpendicularity on a coordinate measuring machine for every first article. The compound route consistently achieves about half the error of the two-machine route. Qingdao Lionse Mechanical Engineering Co., Ltd. provides the first article inspection report with the dimensional results.
3. What Happens to Cycle Time When Turning and Milling Are Combined in One Program?
The cycle time in the compound route includes the same cutting time as the two-machine route, but the non-cutting time is much lower. The non-cutting time includes clamping, alignment, tool change, and transport. In the compound route, the clamping and the alignment are done once. The tool change is done on the same turret or the same tool magazine. The transport between machines is eliminated. The table below shows the cycle time breakdown for a typical part in the two routes.
| Time element | Two-machine route | Compound route |
| Turning cutting time | 8.0 minutes | 8.0 minutes |
| Milling cutting time | 5.5 minutes | 5.5 minutes |
| Clamping and alignment | 6.0 minutes (2 setups) | 2.5 minutes (1 setup) |
| Tool change | 2.0 minutes | 1.2 minutes |
| Transport and queue | 4.0 minutes | 0 minutes |
| Total cycle time per part | 25.5 minutes | 17.2 minutes |
Manufacturing engineer's note: The cycle time reduction in this example is 32 percent. The reduction is not from faster cutting. It is from the elimination of the second clamping, the transport, and the queue. For a batch of 500 parts, the saving is 6,900 minutes, or 115 hours of machine time. In our factory, we calculate the cycle time for each part before quoting, and we recommend the compound route when the non-cutting time is more than 30 percent of the total cycle. Lionse provides the cycle time analysis with the quotation.
4. Why Do Fixture Count and Work-in-Process Inventory Drop With Compound Processing?
Each operation in the traditional route requires its own fixture. A part that goes through turning, milling, drilling, and grinding may need four fixtures. Each fixture must be designed, built, stored, and maintained. The compound route requires one fixture, the main spindle chuck or collet. The fixture cost and the fixture management effort are reduced. The work-in-process inventory also drops because the parts are not waiting between machines. In the traditional route, the parts accumulate in front of the machining center while the lathe finishes the previous batch. In the compound route, the part is completed in one cycle, and the inventory is limited to the parts in the machine and the parts in the inspection area. In our factory, we have measured the work-in-process inventory before and after switching a family of parts to the compound route. The inventory dropped by 60 percent, and the floor space required for the parts dropped by 45 percent.
We also configure the tool turret and the tool holders specifically for the part family. A turn-mill machine with a 12-station turret and a 24-station tool magazine can hold all the tools required for a complex part, so the tool change is done by the program, not by the operator. Qingdao Lionse Mechanical Engineering Co., Ltd. provides the tooling layout and the program for each part family.
5. How Should Engineers Specify and Verify a Compound Processing Route for a Given Part?
The specification should include the part geometry, the tolerance requirements, the material, the batch size, the machine travel, and the number of turret stations. The verification should include three checks. The first is the first article inspection, which measures all the critical features on a coordinate measuring machine. The second is the process capability index, which is calculated from a sample of 30 parts. The third is the cycle time measurement, which is compared with the quoted cycle time. In our factory, we perform the first article inspection and the process capability study for every new part. Qingdao Lionse Mechanical Engineering Co., Ltd. provides the inspection report and the capability index with the first delivery.
We recommend that the designer verify the tool interference before the program is released. A turn-mill machine has more moving elements than a lathe, and a tool that is not properly positioned can collide with the chuck or the tailstock. We use a simulation software to check the tool path and the turret movement before the first cut.
Frequently Asked Questions About CNC Turning Milling Compound Processing
Summary for Manufacturing Engineers and Shop Managers
CNC Turning Milling Compound Processing improves manufacturing efficiency by eliminating the second clamping, reducing the benchmark transfer error, compressing the non-cutting time, and lowering the fixture count and the work-in-process inventory. The improvement is most visible on complex parts with tight tolerances between turned and milled features. The specification should include the part geometry, the tolerances, the batch size, and the machine travel. The verification should include the first article inspection, the process capability index, and the cycle time measurement. Qingdao Lionse Mechanical Engineering Co., Ltd. has been machining precision parts for over 12 years and provides full compound processing evaluation and verification support for our customers.